SUMITOMO EGU positive front corner chip breaker groove
EGU chip breaker core design and characteristics
Double front corner structure (distinguishing design between blade tip and edge)
Blade tip angle section: 5 °+15 ° angle;
Cutting edge cross-section: 3 °+25 °+8 ° composite rake angle; Balancing sharp cutting edges and tool tip impact strength, while balancing low cutting resistance and resistance to chipping.
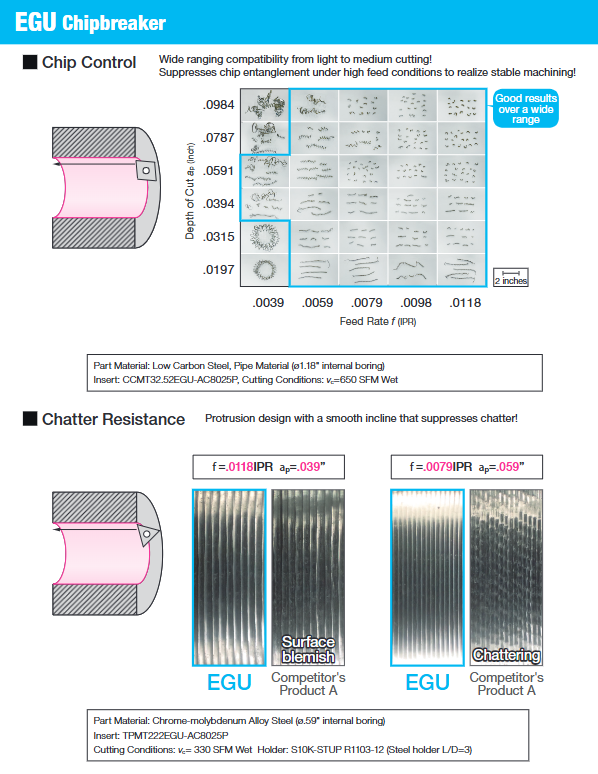
The wide chip accommodating groove and protruding flow guiding structure achieve chip removal and complete chip breaking at the same time; High feed conditions suppress chip entanglement and accumulation, resulting in stable chip morphology.
Excellent anti vibration performance, smooth transition of groove shaped inclined surface, reducing cutting vibration; Compared with competitors, it can eliminate vibration patterns and chatter defects in the weak rigidity working condition of long overhanging boring holes (L/D=3).
Improved anti chipping performance and impact damage test: EGU can withstand 9200 impacts before chipping occurs; Competitor B has only 5700 times and competitor C has only 6200 times; The ability of the blade tip to resist notch damage is significantly better than that of competitors.
Processing condition window feed f ≈ 0.0039-0.0118 IPR; Cut depth ap ≈ 0.020-0.098 inches; Positioning from light cutting to medium cutting.
Comparison of front corner groove types in the same series (ELU/ESU/EGU/EMU)
table
Applicable working conditions for slot positioning
ELU ultra precision machining groove with extremely small cutting depth, micro precision machining, and the smallest window
ESU light cutting precision machining, light load precision machining, small ap, small f
EGU universal main force (recommended in the manual) for light to medium cutting, with the strongest versatility, including inner and outer circles, boring, and profiling
In EMU, the rough machining groove is medium to rough, with a larger cutting depth and feed rate
The EGU window is between ESU and EMU, catering to both precision machining and semi rough machining, and is the universal preferred slot for positive rake angle blades.
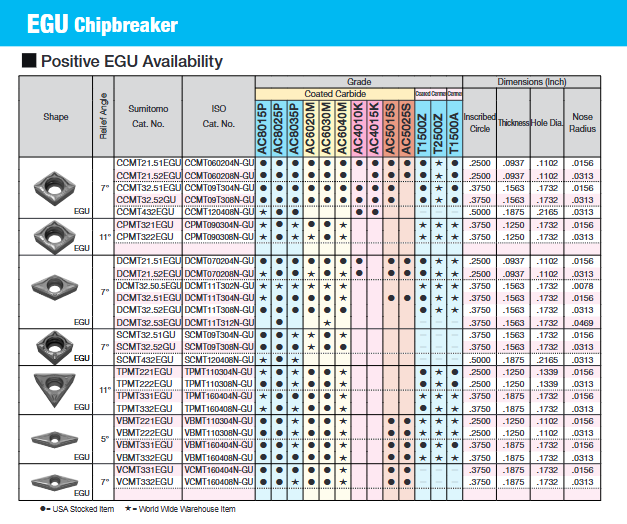
Applicable workpiece materials&compatible grades
Available grades for covering P carbon steel alloy steel/M austenitic stainless steel/K cast iron/S high-temperature alloy (nickel based cobalt based) (fully compatible with the previous manual grade system):
Steel: AC8015P, AC8025P, AC8035P; Metal ceramics T1500A, T1500Z, T2500Z
Stainless steel: AC6020M, AC6030M, AC6040M
Cast iron: AC4010K, AC4015K
High temperature alloys: AC5015S, AC5025S
Recommended cutting parameters (imperial system, mainly wet machining)
Workpiece material grade Vc (SFM) f (IPR) ap (inch)
Soft steel AC8015P/AC8025P/AC8035P; Metal ceramic 525-1375 0.0047-0.0118 0.0197-0.0984
Carbon steel/alloy steel (1045, 4135) AC8015P/AC8025P/AC8035P; Metal ceramic 460-1246 0.0039-0.0118 0.0157-0.0984
Austenitic stainless steel AC6020M/AC6030M/AC6040M 295-690 0.0039-0.0118 0.0157-0.0984
Grey/ductile iron AC4010K/AC4015K 525-2300 0.0039-0.020 0.020-0.240
Nickel based high-temperature alloy AC5015S/AC5025S 80-300 0.0031-0.0098 0.0157-0.0787
Typical applications: Inner hole boring, weakly rigid workpieces, and contour machining.
Actual Processing Cases
Structural steel cylinder body parts, outer circle imitation DCMT32.51EGU-AC8025P: no tool tip failure, better chip removal than traditional groove type.
4130 automotive drive component DCMT32.52EGU-AC8015P: improves chip winding and enhances processing efficiency.
4130 precision mechanical parts, inner hole imitation TPMT221EGU-AC6040M: suppresses tool tip temperature rise and reduces wear and damage.
5015 fastener, inner hole boring CCMT32.52EGU-AC8025P: tool life reaches 1.5 times that of competitors.
4130 automotive parts, inner cone boring CPMT322EGU-AC8025P: eliminates vibration, compared to traditional grooves, there are no vibration patterns under large cutting depths.
52100 bearing steel inner hole boring DCMT32.53EGU-AC8025P: The service life is 1.3 times that of competitors, and the feed adaptability is wide.
Blade product specifications
EGU slot type is used for positive front angle blades (7 °, 11 °, 5 ° rear angle):
80 ° diamond: CCMT series;
55 ° diamond: DCMT series;
Square: SCMT;
Triangle: TPMT;
35 ° diamond shape: VBMT, VCMT;
Blade tip R specification: 0.0078/0.0156/0.0313/0.0469-inch; Inventory Mark: D US Local Spot; Global warehouse transfer.