SUMITOMO PSZ Turn Modular Quick Change Tool System
Core characteristics of the system
Quick change polygon cone positioning structure
Simply loosen one locking screw to replace the entire machining tool head, without the need to remove the entire tool holder from the turret.
X/Y/Z three-axis blade repeat positioning accuracy ≤ 5 μ m; The precision performance in the Y direction (high center of the blade tip) is outstanding, and there is almost no need for compensation after changing the blade.
The rigidity is equivalent to that of an integrated mono block blade, and it will not sacrifice rigidity due to modularity.
Knife shank specifications (metric/imperial square handle)
Metric system: 10 x 10, 12 x 12, 16 x 16, 20 x 20 mm;
Imperial system: 0.375 “, 0.500”, 0.625 “, 0.750”;
The length of the tool holder is 84 mm (10-16 handles) and 100 mm (20 handles); All support internal cooling (- J built-in cooling).
Cooling scheme
The knife holder comes with an internal cooling interface; Support customized integrated cooling blade plate (Gang Plate), plug and play, can switch the cooling pressure (high/low/off) of each tool separately, eliminate exposed hoses, and avoid chip entanglement.
Accessories: Special torque wrench, locking screw (hexagon socket/Torx versions), cooling plug, cooling hose connector; The blade is sold separately.
Auxiliary tool changing fixture: PSZ clamping workstation, offline pre adjustment tool head, external tool alignment, shortening machine downtime.
Naming rules
Example of Knife Rod Body: PSZ1212R-84
PSZ: Series; 1212: Square handle 12 × 12mm; R: Right hand; 84: The total length of the tool holder is 84mm; X represents special customization.
Example of interchangeable blade: PSZ12-K-SCLCR-0616-06
PSZ12: compatible with 12mm tool holder; K: Interchangeable blade head; SCLCR: Knife head type; 0616: WF LH size; 06: Blade model code.
All interchangeable blade types
1) Ordinary outer circle/end face/profile turning (ISO standard blade)
Blade code, main angle blade type, and purpose
SCLC-R/L 95 ° CCMT (80 ° diamond front angle) outer circle+end face turning
SDHC-R/L 107.5 ° DCMT (55 ° diamond front angle) multifunctional contour machining
SDJC-R/L 93 ° DCMT outer circle contour imitation
SVJB-R/L 93 ° VBMT (35 ° diamond front angle) profile, small angle contour
SVHC-R/L 107.5 ° VCMT copying
SVJC-R/L 93 ° VCMT contour contouring
PCLN-R/L 95 ° CNMG negative rake angle blade heavy load outer circular end face turning
PDJN-R/L 93 ° DNMG negative rake angle blade negative rake angle blade imitation
Compatible grades: AC8025P, AC6030M, AC1030U, AC1135U, AC5015S, etc; Compatible with all positive front corner chip breakers such as EGU/ELU/ESU/EMU.
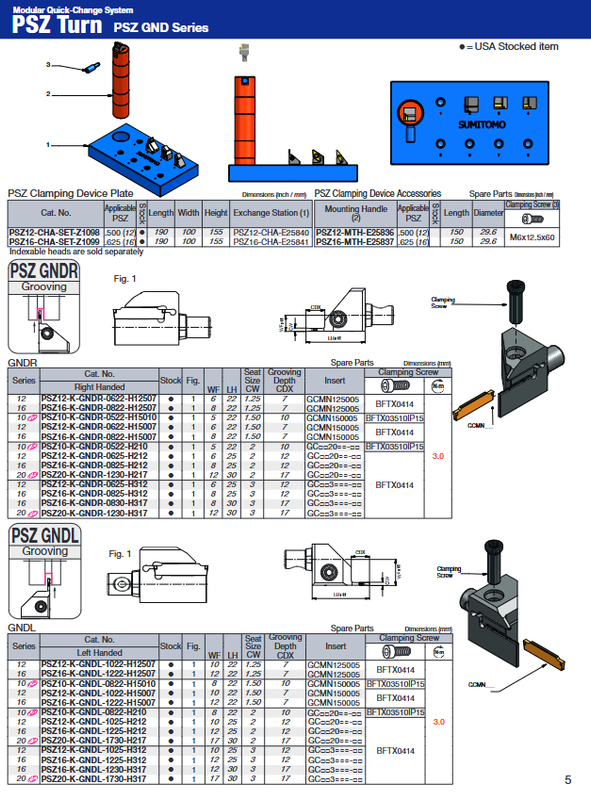
2) GND slot cutting blade PSZ-K-GNDR/GNDL (right-hand/left-hand)
Directly compatible with GCMN series GND slot cutting blades, with a slot width of 1.25-3mm.
Maximum cutting depth CDX: 7 ~17 mm; suitable for cutting grooves on the outer circle of the walking machine.
All GND slot types such as MG, ML, GG, CG can be used, and the brand is completely compatible with the GND manual.
3) SBT Back Turning Tool Head PSZ-K-SBT3/5/8-R
Special tool head for reverse turning; Use BTR specific back car blades.
Blade specifications BTR35/BTR55/BTR80, maximum back depth 3.82mm/5.88mm/8.83mm.
Applicable: Reverse chamfering of the rear end of the shaft, back turning tool groove; Blade materials AC1030U, AC5015S, AC530U, etc; Recommend oil-based cooling.
4) ER external thread cutting head PSZ-K-ER
Use 16ER standard external thread blades; Support: metric ISO, US UN, Wyeth 55 ° pipe thread, NPT/BSPT cone pipe thread, UNJ reinforced thread; Partial full tooth/partial tooth blade.
The main brand is AC530U.
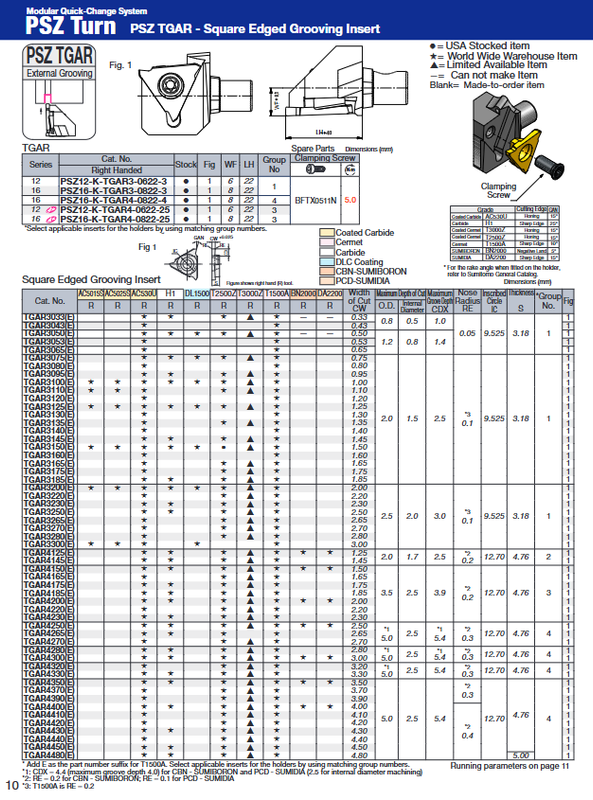
5) TGAR slotting blade PSZ-K-TGAR
The triangular blade cutting system is divided into right angle groove blade TGAR (flat groove) and arc groove TGAR-R; Blade width is 0.33~4.80mm.
The blade material covers hard alloy, metal ceramic T1500A/T2500Z, CBN BN2000, PCD DA2200, and can process steel, stainless steel, high-temperature alloys, quenched steel, and non-ferrous metals.
It is also compatible with TTE thread inserts for thread processing.
Summary of applicable blade grades (integrated with the previous manual)
Steel: AC8015P, AC8025P, AC8035P, metal ceramic T1500A/T2500Z
Stainless steel small parts: AC1030U, AC1135U; Universal stainless steel AC6020M/AC6030M
High temperature alloys: AC5015S, AC5025S
Cast iron: AC4010K, AC4015K
Hard material: CBN BN2000; Nonferrous metals: PCD DA2200, uncoated H1
Key usage points
Torque requirement: The locking screws of different handle numbers have specified torque, and Sumitomo’s dedicated torque wrench must be used. Insufficient torque will result in loss of positioning accuracy, and excessive torque will damage the threads.
The polygonal cone surface must be kept clean, as iron filings can directly damage the 5 μ m repeatability accuracy.
Integrated cutting plate Gang Plate: suitable for the cutting tower of the walking machine, with the tool holder body left on the cutting plate and only the front blade head replaced, greatly reducing tool changing/debugging time; The internal cooling pipeline is integrated inside the blade plate, eliminating the need for external hoses.
The height of the SBT back turning tool holder should have a positive tolerance of+0.1~+0.3 mm to prevent the tool body from interfering with the workpiece.
TGAR blade heads must be matched with Group group numbers and cannot be mixed across groups.
Applicable devices and scenarios
✅ Sliding spindle walking machine, multi axis automatic lathe;
✅ Batch small items: outer circle, end face, contour imitation; Cutting off the outer circular groove; Carrying a car; External thread;
✅ External pre adjustment reduces machine downtime and is suitable for frequent changeover production of multiple varieties;
✅ Internal cooling supports high-pressure cooling, improving the service life of stainless steel and high-temperature alloy cutting tools.