

SUMITOMO ELECTRIC AC1030U Material Blade
Core features and advantages of the product
Coating and substrate structure
New multi-layer PVD coating (Absotech Bronze): 4-layer functional structure 1) Smooth anti collapse layer: achieving excellent workpiece surface quality; 2) High hardness heat-resistant layer: enhances wear resistance; 3) High adhesion technology: prevents coating peeling off; 4) Strong and tough hard alloy matrix: significantly resistant to chipping.
Compared to conventional blades and competitor blades: AC1030U blades have no breakage after processing; Competitors and ordinary brands have coating defects.
Excellent surface quality during processing
The blade has undergone high-quality edge grinding, with an Rz of 0.65 μ m for AC1030U; Ordinary grade Rz=1.20 μ m.
4137 steel outer circle precision machining test: AC1030U without tearing, Rz=2.0μm; The ordinary blade Rz=4.1 μ m and the competitor Rz=4.3 μ m both have machining tear defects.
It can suppress micro chipping and material adhesion, greatly improving the roughness of the processed surface.
The applicable cutting speed SFM range for machining intervals is about 165-650SFM, suitable for high-precision machining scenarios. Compared with other Sumitomo grades such as AC520U, AC530U, AC6040M, ACZ150, AC1030U focuses on high-precision precision machining of small parts.
Recommended cutting parameters (in English units SFM/IPR)
Processing material cutting speed Vc (SFM) feed f (IPR)
Soft steel 165-500 0.0008-0.006
Carbon steel 165-500 0.0008-0.004
Stainless steel 165-500 0.0008-0.004
Brass 230-1000 0.002-0.008
Cast iron 160-650 0.0008-0.004
Special alloy 100-200 0.0008-0.004
The processing conditions are generally wet cooling.
Actual Processing Cases
304 stainless steel processing: Vc=330SFM, f=0.002IPR, ap=0.004 “; AC1030U has less wear on the back cutting surface, and the Rz roughness of the workpiece is maintained at a low level throughout the process, with better stability than ordinary blades and competitors.
1047 steel stator shaft: AC1030U single blade can process 140 pieces, while ordinary blades can only process 70 pieces.
304 stainless steel valve body; 430 stainless steel sensor housing: AC1030U can process 1600 pieces, while ordinary blades only have 800 pieces, significantly improving the lifespan of individual cutting tools.
Introduction to chip breaker
The manual is divided into two categories: Handed Chipbreakers and Neutral Chipbreakers, providing applicable cutting depth and feed window diagrams for each slot type.
FX/FY/FYS (Left and Right Hand Slot Type)
FYS: For soft materials, improve chip removal, resist crescent wear, reduce edge damage, suitable for fine cutting, 15 ° groove angle.
FY and FX are used for precision machining of outer circles/inner holes with different feed cutting depths.
MESI/(M) EFC/(M) EFM (Neutral Slot Type)
Code prefix M: represents negative tolerance tool tip radius.
EFC, EFM, and MESI are suitable for neutral and non directional precision turning.
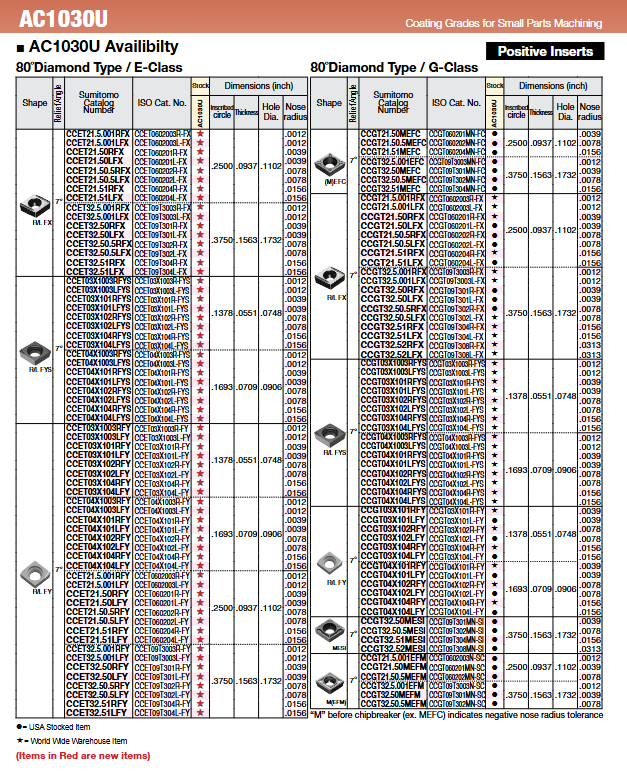
Blade product specifications (AC1030U available models)
Tag description: l=US local inventory spot; Global warehouse transfer; Red=newly developed model; It is divided into positive front angle blades, negative front angle blades, and specialized blades for small hole boring and cutting grooves.
1) Positive Insertions
80 ° diamond shape: CCET/CCGT (E-class, G-class tolerances); Slot FX, FYS, FY, MESI, MEFC, MEFM
55 ° diamond shape: DCET/DCGT; Slot FX, FYS, FY, MESI, MEFC
Square: SCGT
Triangle: TBGT, TCGT, TPGT
35 ° diamond: VBET, VCET, VPET, VBGT, VCGT; Small parts precision turning is commonly used.
2) Negative inserts
55 ° diamond shaped DNGG, 35 ° diamond shaped VNGG, triangular TNGG; Slot type FY, FX.
3) Small knife handle specialized blade
MINI boring tool blades KBMX/KBMZ/KBMG: extremely small aperture machining, minimum machining aperture DMIN=1.0mm; Includes external boring, reverse inner hole turning, inner hole slotting blades, compatible with CKB boring bar.
SCT cutting blade CTR/CTL: a small cutting blade with a maximum cutting diameter of 5-16mm, divided into right-handed and left-handed versions, with or without a chip breaker.
GCM/GXMN slotting cutting blade: GND/GNDIS shank, inch specifications; CF, ML, GF various groove types.
SUMIGRIP (WCFN/WCFR/WCFL): Special alloy low feed groove with a cutting width of 2-5mm.
Applicable workpiece scenarios
Suitable for small precision parts: valve body, sensor housing, motor shaft, small shaft type; The material covers carbon steel, alloy steel, stainless steel, brass, cast iron, and some special alloys; Suitable for precision machining of walking machines and small CNC lathes.


