SUMITOMO AC6000M series (AC6020M/AC6030M/AC6135M/AC6145M) stainless steel turning
Four brand positioning and coating technologies
Brand coating type, core positioning performance, focusing on applicable working conditions
AC6020M CVD precision machining/high-speed machining grade, high wear resistance, anti stick knife stainless steel precision machining, high-speed continuous cutting
AC6030M CVD continuous cutting is the preferred main grade for wear-resistant and anti adhesion balance, suppressing abnormal collapse. Austenitic stainless steel continuous turning, precision semi precision, universal continuous working conditions
AC6135M (new) PVD mild intermittent, mill scale processing wear-resistant and fracture resistant balance with oxidized fur billet, mild intermittent, semi precision medium cutting
AC6145M (new) PVD heavy intermittent processing grade with extremely high toughness, resistance to chipping, strong impact, large gap, heavy intermittent rough processing
Principles of Coating Technology
CVD grades AC6020M/AC6030M use ABS TECH CVD: TiCN+high toughness Al ₂ O Ⅲ alumina layer, combined with surface smoothing treatment process; Reduce the adhesion of workpiece materials, suppress blade breakage caused by sticking knives, and achieve high bonding strength at the coating substrate interface.
PVD grades AC6135M/AC6145M (new replacement for old AC6040M) adopt TiAlBCN based multi-layer PVD coating system:
Lubricate TiCN anti adhesion layer: inhibit stainless steel bonding;
High hardness TiAlN multi-layer wear-resistant layer: resistant to crescent shaped grooves and rear blade wear;
Ultra fine grain TiAlN anti collapse layer: prevents sudden blade collapse;
High adhesion technology enhances the bonding strength of coatings; AC6145M is equipped with a high toughness hard alloy matrix.
Applicable materials: ferritic, martensitic, austenitic 304/316, duplex stainless steel, precipitation hardened stainless steel.
Complete chip breaker system (with negative front angle as the main feature, and new EEH slots added)
Slot type code, processing grade, core characteristics, recommended use
ESU precision machining with small cutting depth, low cutting resistance, and small margin precision turning
EEF precision machining excellent chip removal, preferred for small cutting deep precision machining
EEX precision – light to medium cutting surface groove reduces cutting heat and cutting load, precision to semi precision transition
EUP light medium cutting double positive rake angle, sharp edge, high feed for light cutting
EGU medium cutting [universal preferred for all series] spherical protrusion, wide chip removal window, comprehensive balance of the majority of stainless steel outer circular end faces, recommended groove type as the first sample
EEG medium cutting focuses on wear resistance, stable chip removal, and moderate load, pursuing long life
EEH (New) Medium Coarse Machining (Intermittent Special) Double Step Front Angle, Impact Resistance, Suppressing Collapse Intermittent Machining Preferred, AC6135M/AC6145M Main Groove Type
EEM rough machining with large cutting depth and feed rate, high blade strength, stainless steel rough lathe
Selection logic: Choose ESU/EEF for small and deep cuts; General working condition priority EGU; Intermittent priority EEH; Choose EEM for heavy load rough machining.
Performance test results (wet cooling)
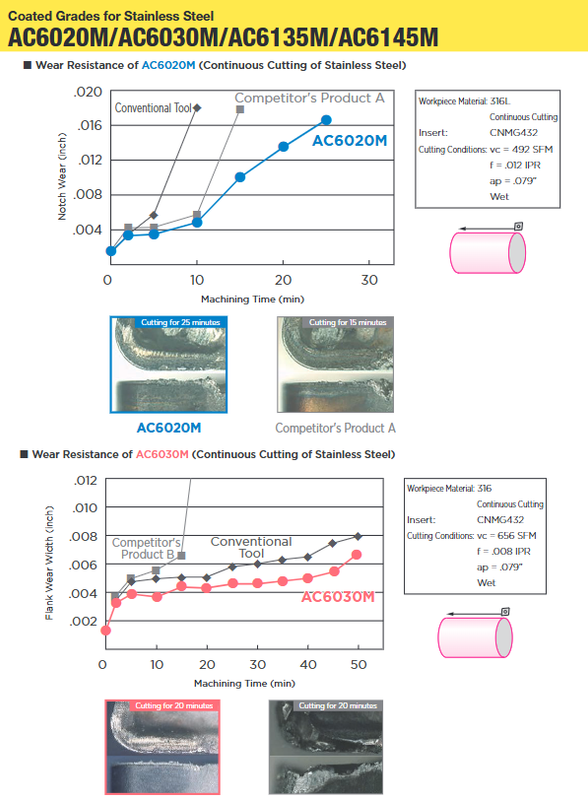
AC6020M, 316L continuous cutting: The anti groove wear ability is significantly better than competitors, the tool life is three times that of traditional grades, and the anti chipping edge is increased by 30%.
AC6030M, 316 continuous cutting: suppresses stainless steel sticking to the tool, with a lifespan twice that of competitors under the same conditions, supporting higher cutting efficiency.
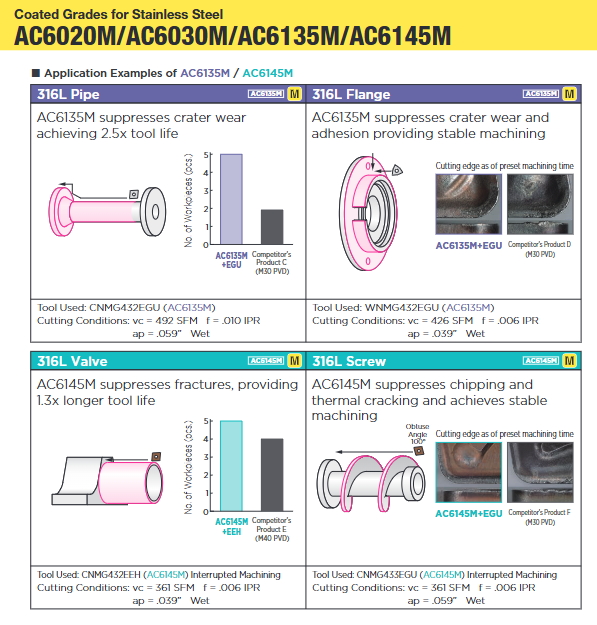
AC6135M, 316 mild intermittent: resistant to crescent wear, with a lifespan of 2.5 times that of the competitor M30-PVD, and stable performance of the rough with oxide skin.
AC6145M, 316 intermittent impact test: withstands far more impacts than traditional cutting tools and competitor M40-PVD, suppressing hot cracking and breakage; The lifespan of intermittent working conditions is increased by 1.3 times.
Recommended cutting parameters (imperial, wet preferred)
Workpiece material working condition priority groove type grade ap (in) f (IPR) Vc (SFM)
Ferritic stainless steel precision machining EEF/ESU AC6020M 0.020-0.079 0.002-0.010 558-984
Ferritic stainless steel continuous EEG/EGU/EEX AC6030M 0.039-0.157 0.004-0.016 459-820
Ferritic stainless steel light intermittent/rolled EGU/EEH AC6135M 0.039-0.197 0.008-0.020 459-656
Ferritic stainless steel with heavy intermittent EEH/EEM AC6145M 0.059-0.236 0.010-0.024 328-525
Martensitic stainless steel precision machining EEF/ESU AC6020M 0.020-0.079 0.002-0.010 394-787
Martensitic stainless steel continuous EEG/EGU/EEX AC6030M 0.039-0.157 0.004-0.016 328-656
Martensitic stainless steel light intermittent/rolled EGU/EEH AC6135M 0.039-0.197 0.008-0.020 262-591
Martensitic stainless steel with heavy intermittent EEH/EEM AC6145M 0.059-0.236 0.010-0.024 197-459
Austenitic stainless steel 304/316 precision machined EEF/ESU/EEX AC6030M 0.020-0.079 0.002-0.010 394-787
Austenitic stainless steel 304/316 continuous EEG/EGU AC6135M 0.039-0.157 0.004-0.016 328-656
Austenitic stainless steel 304/316 light intermittent/rolled EGU/EEH AC6135M 0.039-0.197 0.008-0.020 262-591
Austenitic stainless steel 304/316 heavy intermittent EEH/EEM AC6145M 0.059-0.236 0.010-0.024 197-459
Double phase stainless steel precision machining EEF/ESU/EX AC6030M 0.020-0.079 0.002-0.010 328-591
Dual phase stainless steel continuous EEG/EGU AC6135M 0.039-0.157 0.004-0.016 262-525
Dual phase stainless steel light intermittent/rolled EGU/EEH AC6135M 0.039-0.197 0.008-0.020 230-459
Double phase stainless steel heavy intermittent EEH/EEM AC6145M 0.059-0.236 0.010-0.024 164-394
Precipitation hardening stainless steel precision machining EEF/ESU AC6020M 0.020-0.079 0.002-0.010 295-459
Precipitation hardening stainless steel continuous EEG/EGU/EEX AC6030M 0.039-0.157 0.004-0.016 230-427
Precipitation hardening stainless steel with light intermittent/rolling EGU/EEH AC6135M 0.039-0.197 0.008-0.020 164-394
Precipitation hardening stainless steel with heavy intermittent EEH/EEM AC6145M 0.059-0.236 0.010-0.024 131-328
Red indicates the recommended parameters for document priority; It is strongly recommended to have sufficient wet cooling for stainless steel processing.
Actual Processing Cases
AC6020M
316L shell (continuous turning, EGU groove): lifespan is three times that of traditional M20 grade;
Stainless steel parts: anti chipping blades, increased lifespan by 30%.
AC6030M
Casting stainless steel pump parts (EEF precision machining): doubled lifespan;
430 Motorcycle Parts (EEG): Cutting efficiency increased by 2.5 times, while tool life doubled.
AC6135M (with oxide skin/mild intermittent)
316L pipeline (EGU): suppresses crescent wear and has a lifespan 2.5 times that of the competitor M30-PVD;
316L flange parts: anti adhesive, stable processing state.
AC6145M (heavy intermittent)
316L valve, EEH intermittent groove: suppresses collapse and increases lifespan by 1.3 times;
Intermittent turning of 316L screws: suppresses chipping and hot cracking, ensuring stable machining.
Overview of Blade Specifications
Marking description: Local spot goods in the United States; Global warehouse transfer.
Negative rake angle blade (mainstream for stainless steel turning)
80 ° diamond shape: CNMG, CNMM;
55 ° diamond shape: DNMG;
Square: SGMG, SGMM;
Triangle: TNMG;
35 ° diamond shape: VNMG;
Trigon:WNMG。 Slot type coverage: EFB/EFE/ELU/ESU/EEF/EEE/EUP/EGU/EEG/EEH (new intermittent slots)/EM/EMU/ENP/EHM, etc.
Positive front angle blade (7 °/11 ° rear angle, suitable for small parts of walking machines)
80 ° diamond shaped CCGT/CCMT/CPMT; 55 ° diamond shaped DCGT/DCMT/DPMT;
Square SCMT/SPMT; Triangle TCMT/TPMT; 35 ° diamond shaped VCGT/VCMT/VPGT;
Slot types: MESI, ELB, ELU, ESU, EGU, EMU, etc., compatible with small part machining of walking machines.